Precision-engineered intermediate chemicals tailored for specialized applications across agrochemicals, polymers, and active pharmaceutical ingredient (API) synthesis.
The Grenville regional industrial sector is experiencing a period of strategic modernization. As local enterprises expand their footprint in agricultural formulations, specialty polymer processing, advanced coatings, and pharmaceutical synthesis, demand for robust, high-purity organic intermediates has hit an all-time high.
Grenville’s regional manufacturing infrastructure relies on consistent access to core building blocks like alkylating agents, halogenated aromatics, specialty amides, and fluorinated compounds. Local buyers require suppliers who understand the strict regional environmental directives, volatile transport timelines, and stringent impurity tolerances demanded by modern end-products. Providing direct chemical supply routes from major synthesis clusters to Grenville allows local facilities to streamline inventory holding costs while mitigating supply disruption risks.
On a global scale, the organic chemistry market is undergoing structural realignment driven by stringent ESG (Environmental, Social, and Governance) mandates, fluctuating petroleum feedstock prices, and tighter regulatory scrutiny under REACH and EPA standards. Fine chemical buyers worldwide can no longer rely on single-source local distributors who stock small volumes at significant markups.
The global trend favors direct, vertically integrated partnerships with primary chemical manufacturers. Chemical synthesis requires high capital efficiency, advanced waste-treatment infrastructure, and continuous flow micro-reactor capabilities to keep unit costs low while eliminating batch-to-batch variance.
Adopting continuous flow reactors, green catalysis, and solvent recycling to drastically reduce VOC emissions and energy consumption.
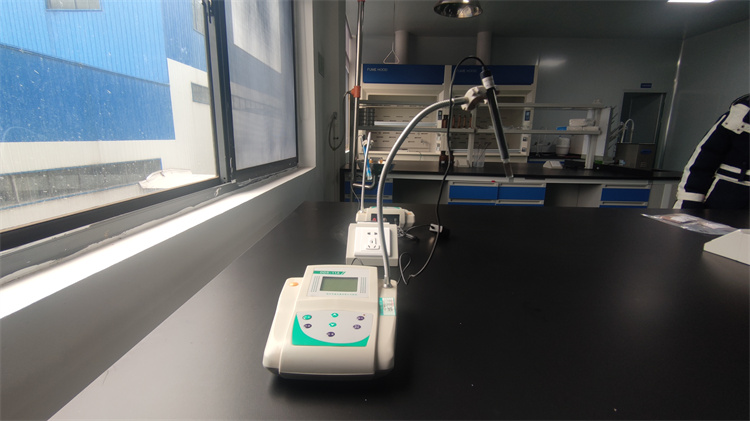
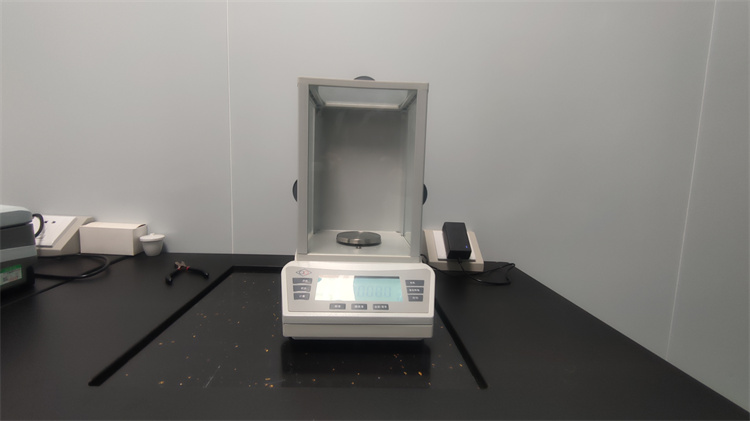
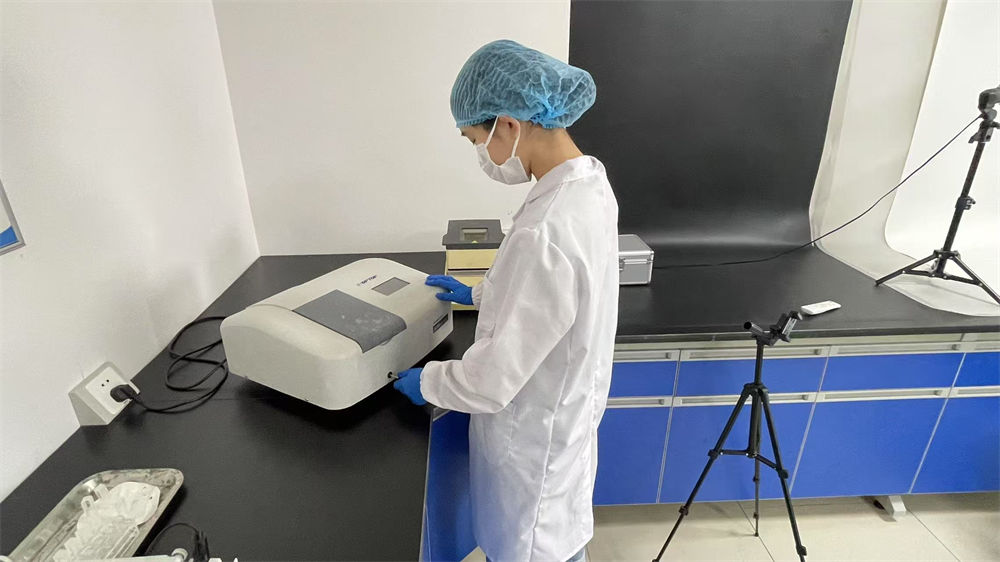
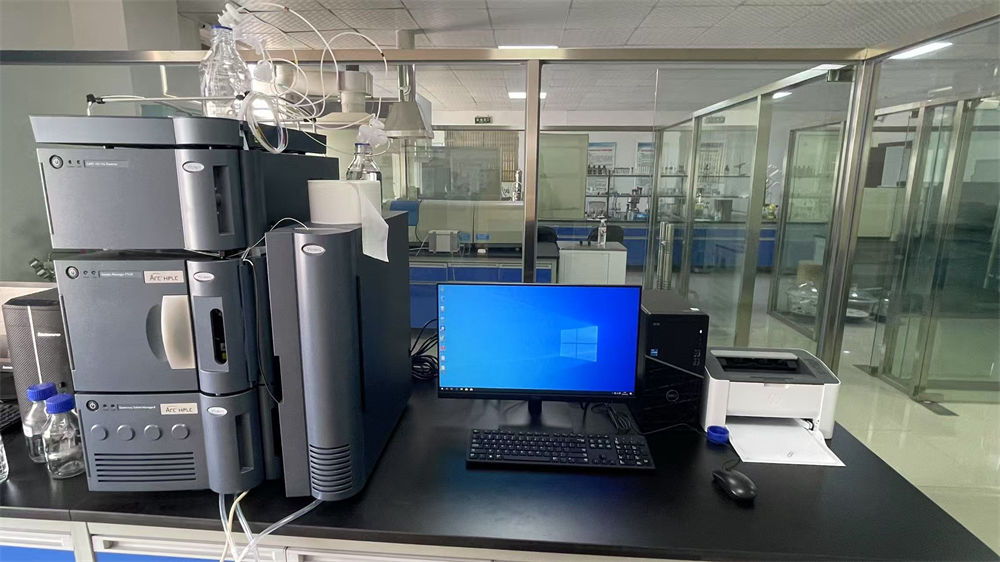
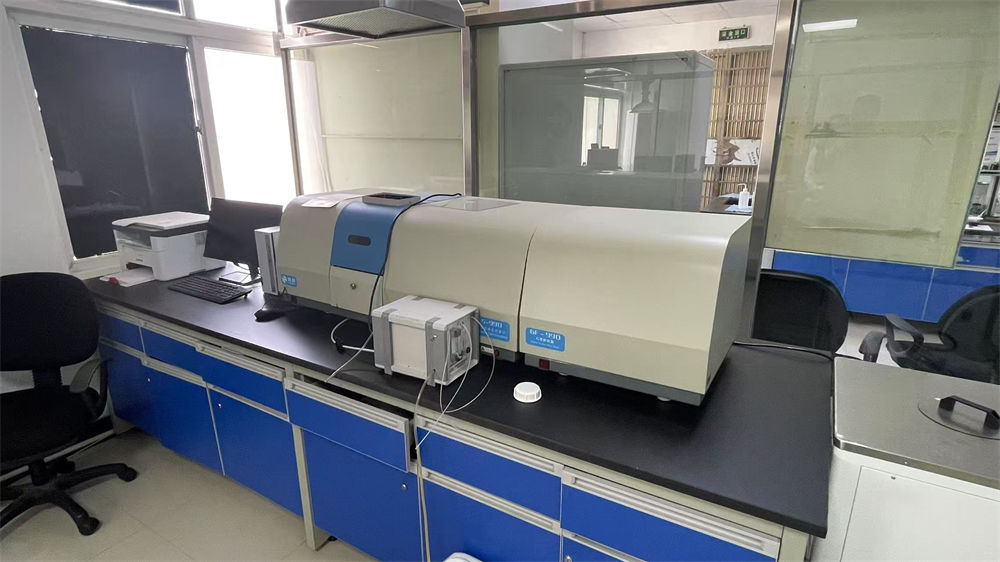
Ultra-precise trace impurity identification using advanced HPLC, GC-MS, and LC-MS instruments to meet strict international standards.
Integrated sea and air chemical logistics with temperature-controlled shipping containers delivered reliably into Grenville port hubs.
China hosts the world's most integrated chemical manufacturing supply chains. From raw petrochemical refining to complex multi-step custom organic synthesis, our localized raw material density means synthesis routes are never delayed by basic chemical availability. This allows us to offer Grenville clients unmatched price stability and contract reliability.
Modern Chinese chemical plants operate with high-level process automation, continuous crystallization technology, and automated reaction control systems. By optimizing molar yields and reclaiming heat and reaction side-products, our facilities minimize per-kilogram overhead while maximizing purity consistency across multi-ton production runs.
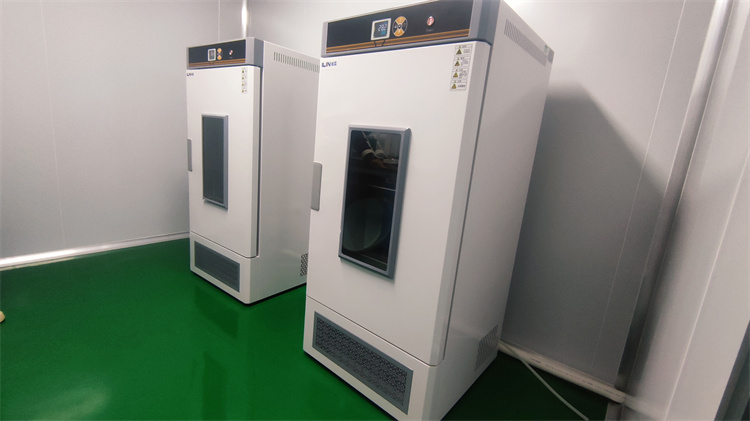
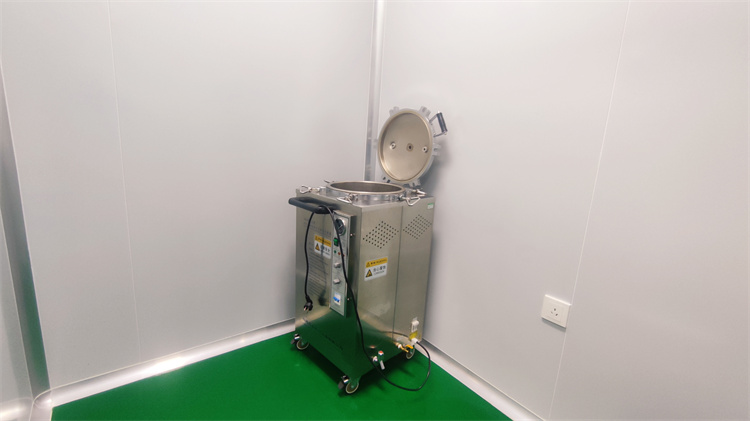
Every batch dispatched to Grenville undergoes comprehensive analytical testing to guarantee compliance with exact physical and chemical specifications.
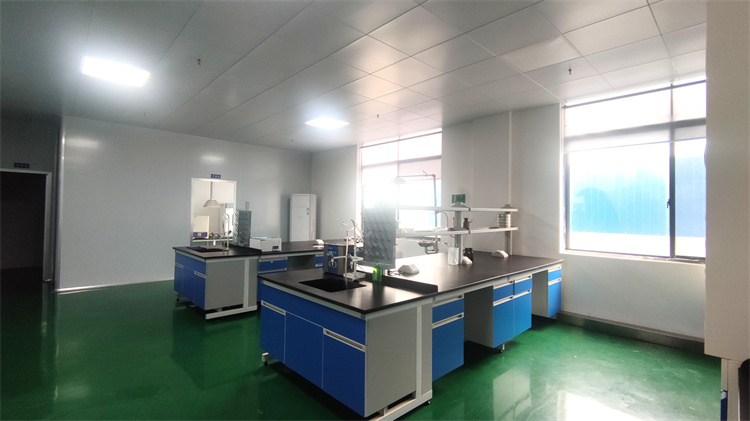
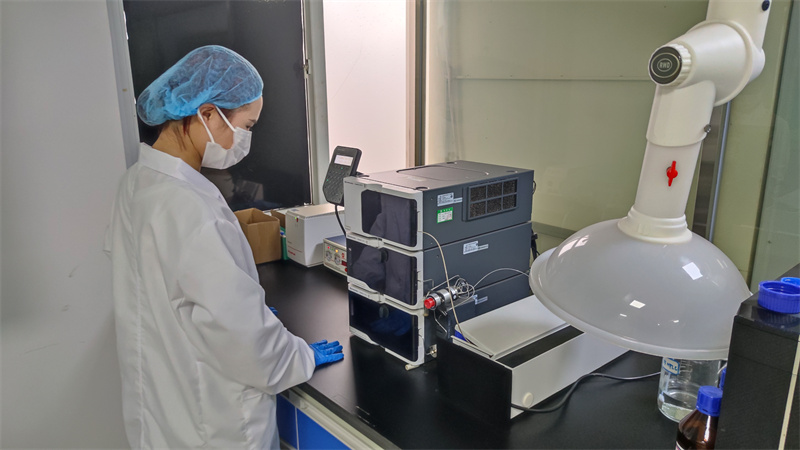
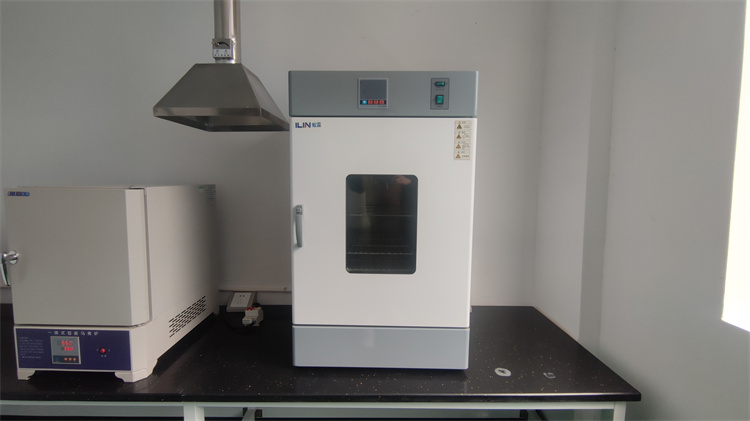
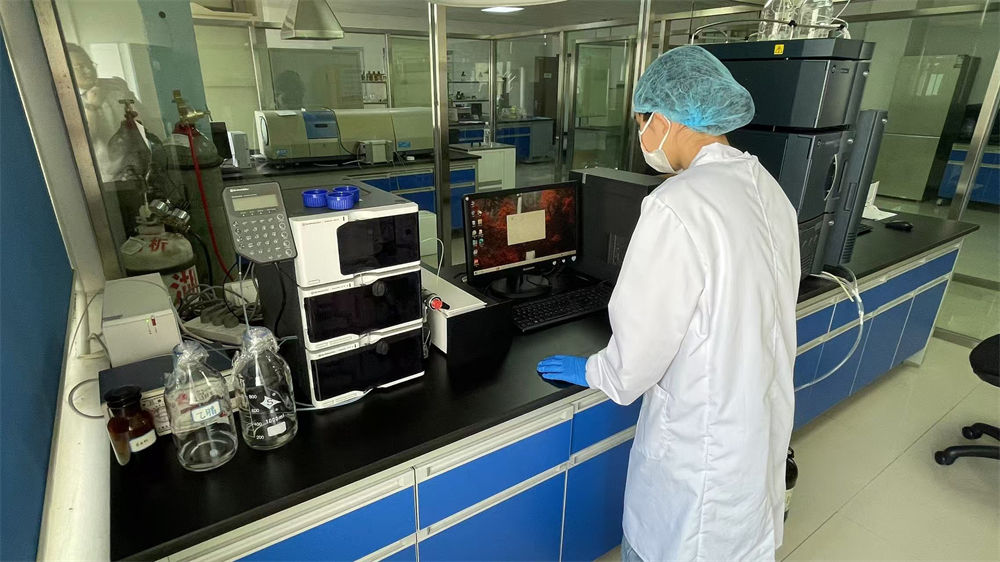
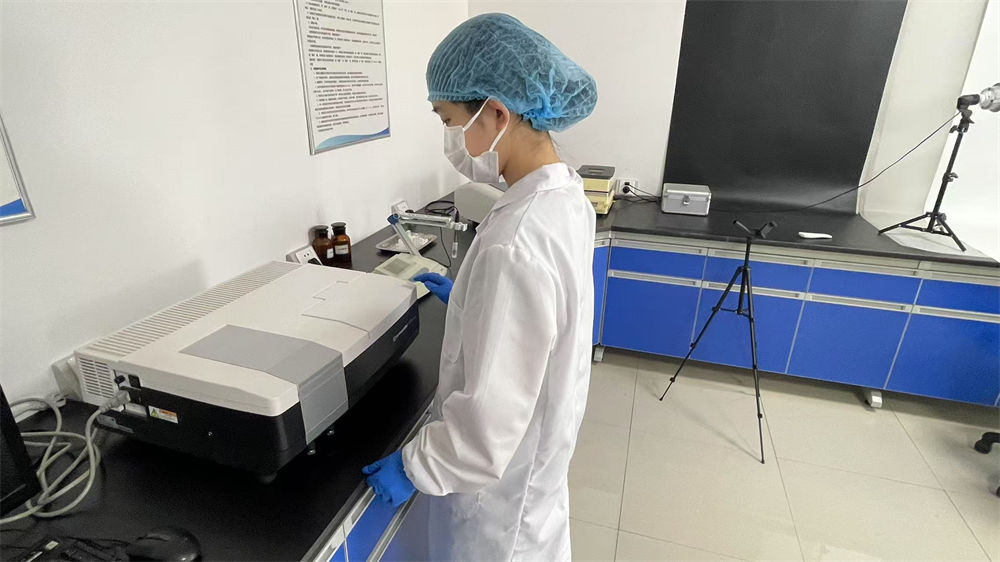
How our fine chemical intermediates fuel growth in Grenville’s core industrial segments.
Precision chlorotoluenes and fluorinated intermediates act as key precursor building blocks for crop protection chemicals, fungicides, and selective herbicides adapted for regional agricultural land management.
Sulfonamides, substituted cyclopropanols, and functionalized amides serve as critical API precursors, manufactured under tight cleanroom standards for custom pharmaceutical formulators.
Organic initiators like Benzoyl Peroxide (BPO) and slip agents like Erucamide provide controlled polymerization rates and surface friction modification for advanced film extruders in Grenville.
Shanghai Aeterna Biotech Co., Ltd. is a leading, reliable, and professional manufacturer specializing in fine chemicals, plant extracts, enzyme preparations, and nutritional ingredients. Our expertise spans research, development, production, and global sales. With decades of experience, we have built a solid reputation for delivering high-quality products and innovative solutions to a wide range of industries including the Grenville market.
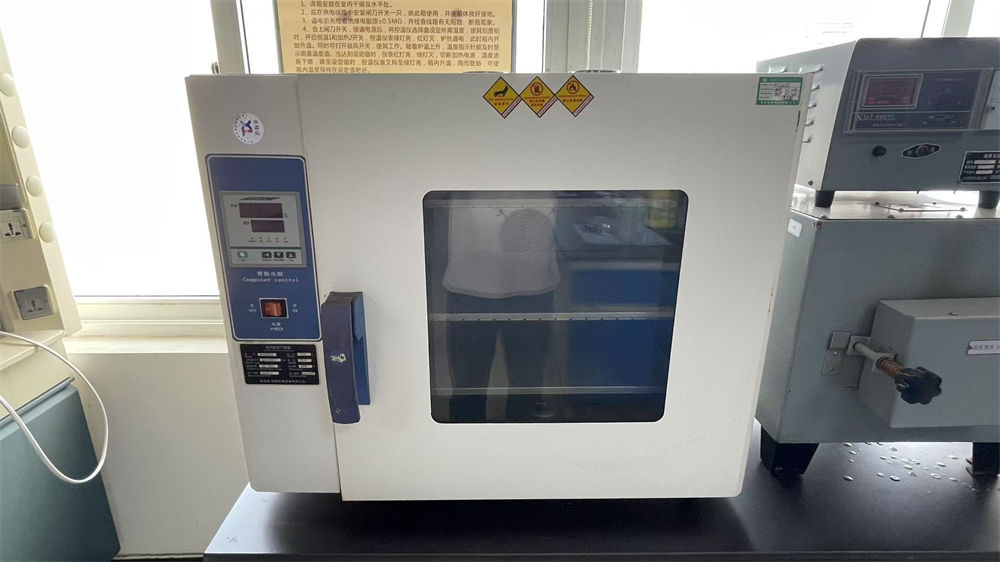
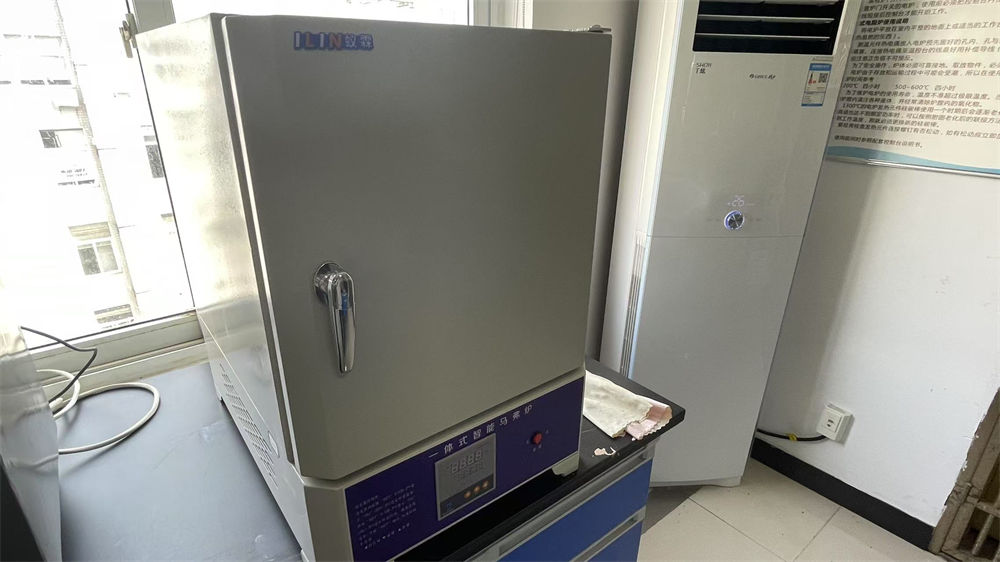
Our facilities are equipped with state-of-the-art production and testing equipment, allowing us to meet the highest industry standards. Through years of serving European and American markets, our QA/QC team has gained extensive experience in impurity analysis, precise control of flavor and fragrance formulations, and rigorous quality management. Our commitment to safety and reliability ensures that every product meets the expectations of both clients and end consumers.
With modern production facilities and advanced logistics, Shanghai Aeterna Biotech manufactures thousands of tons of premium products annually. Our close partnerships with major international freight forwarders in Shanghai ensure timely global distribution. The integration of China’s advanced Logistics Information Management System enables us to provide fast, reliable, and cost-effective shipping solutions for our clients worldwide.
Over the years, our commitment to quality, professionalism, and customer satisfaction has allowed Shanghai Aeterna Biotech to evolve from a small-scale manufacturer into a globally recognized supplier and one-stop solution provider. We serve customers across Europe, North America, Asia, and other regions, offering tailored solutions that meet their specific requirements.
At Shanghai Aeterna Biotech, we uphold the principles of credibility, integrity, and long-term partnership. Our goal is to provide:
We sincerely invite your esteemed company to explore cooperation with us and experience our professional service. Together, we can create a brighter future through innovation, reliability, and mutual success.
Explore our comprehensive chemical inventory. Click any item for full chemical specs, CAS numbers, and bulk purchasing inquiries.
Each batch undergoes rigorous analytical testing including HPLC (High-Performance Liquid Chromatography), GC-MS, and moisture/ash analysis. A Certificate of Analysis (COA) matching exact customer specifications is issued prior to dispatch.
Standard catalog items ship within 7-10 business days from our Shanghai logistics hub. Transit to Grenville ports takes approximately 18-25 days depending on shipping line selection and customs clearance speed.
Yes, our R&D center specializes in custom scale-up synthesis from bench-scale grams to multi-ton reaction batches. We customize purity levels, solvent residues, and physical forms (powder, liquid, granulate) per client request.
We supply UN-certified steel drums, IBC totes, fluorinated HDPE containers, and vacuum-sealed bags with nitrogen purging for air- or moisture-sensitive intermediates to ensure safety during sea freight.
Connect directly with our engineering and procurement team to discuss technical specifications, pricing tiers, COA verification, and sample delivery for your upcoming production schedule.
Send Inquiry Now Aeterna Biotech